


Keep Material Moving with Confidence
Conveyors are the backbone of efficient material flow, helping material move reliably between processes while creating consistency and reducing manual handling. Adaptec engineers and integrates custom conveyor systems for a wide range of industries and applications, including manufacturing, end-of-line packaging, distribution, and order fulfillment. With a focus on increasing throughput and improving efficiency, we work closely with you to understand your application requirements and operational goals to deliver solutions that keep material moving.

Improved Throughput
Reduced Manual Handling
Optimized Facility Flow
Scalable System Integration
Engineering systems that keep business moving.
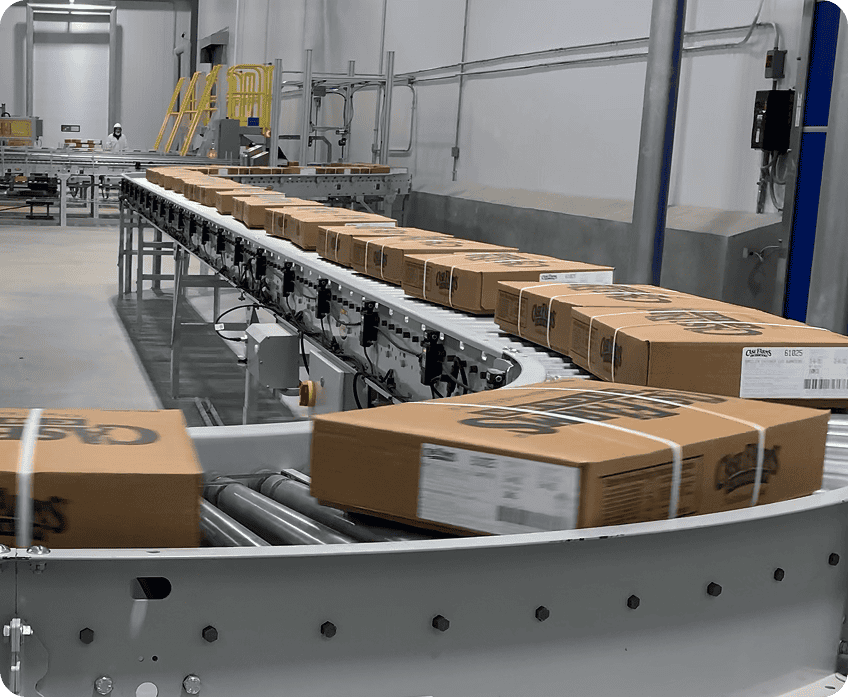
Types of Conveyor Systems
Accumulation conveyors are a type of material handling conveyor used to temporarily store and accumulate items or products at various points along a production or distribution line. Unlike standard conveyors, which move items continuously, accumulation conveyors allow for the controlled accumulation of products until they are ready for further processing or packaging.
Main Usages
- Buffering product between order selection and order assembly
- Merging multiple conveyors into a single stream
- Loading conveyors for route delivery or building orders from multiple areas
- Smoothing irregularities between processes in an operation
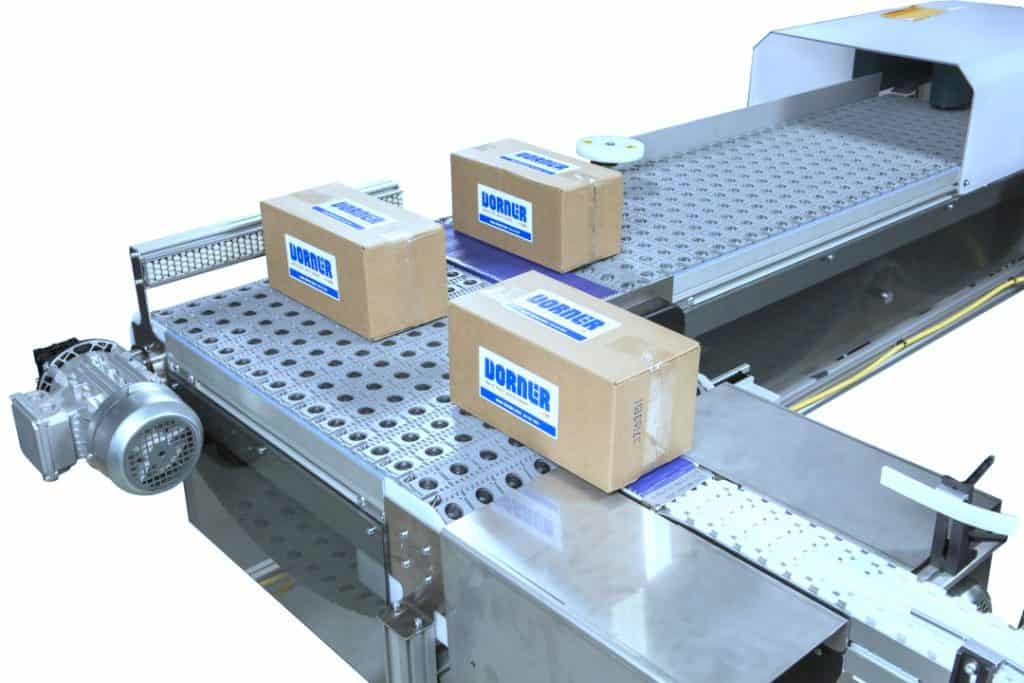
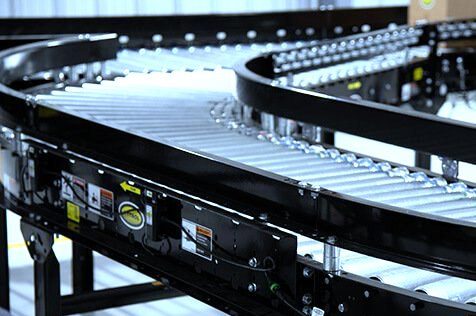
Activated Roller Belt (ARB) conveyors are an innovative solution for superior package manipulation, minimizing floor space consumption and providing flexibility to handle multiple product sizes without the need for changeover. ARB conveyor technology improves productivity by eliminating unnecessary labor costs while reducing operational expenses in many package handling applications. ARB is a low maintenance solution for increasing system reliability.
Main Usages
- Singulation after robotic depalletizing
- Package alignment and centering
- Merging, switching or sortation
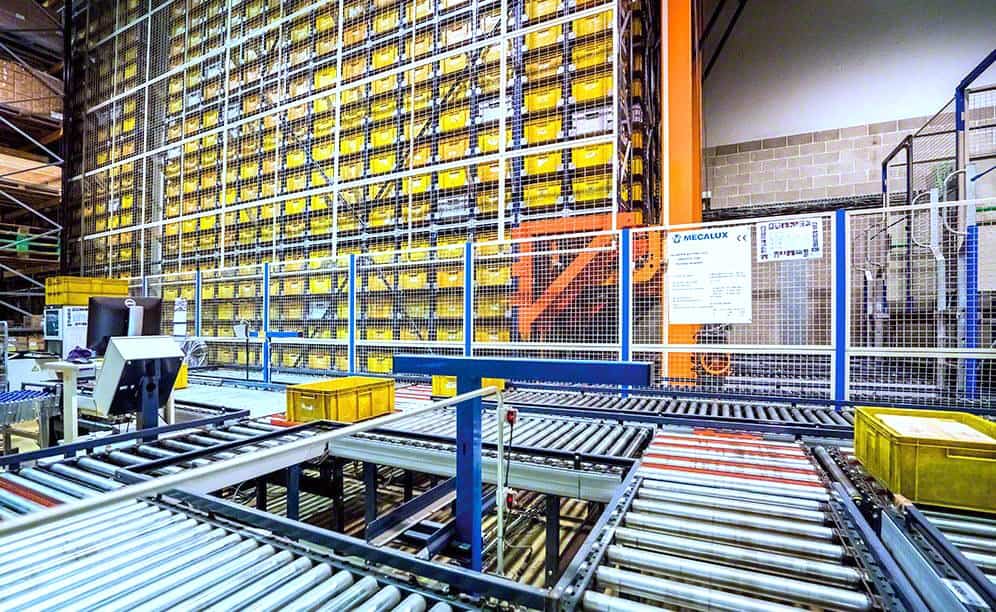
Automated case flow is the conveyor technology and integration which merges and sorts multiple product SKUs into single, or multiple, conveyor lines at varying patterns based on the output need. These systems are optimal for distribution facilities needing to send product in a conveyor line to palletizing systems for mixed pallet loads.
We custom engineer automated case flow system solutions unique to your needs using conveyors and software from our top of the line conveyor manufacturer partners.
Main Usages
- High-Speed Case Handling with Product Tracking
- Merging and Diverting Product Flow
- Synchronizing Automated Packaging Systems
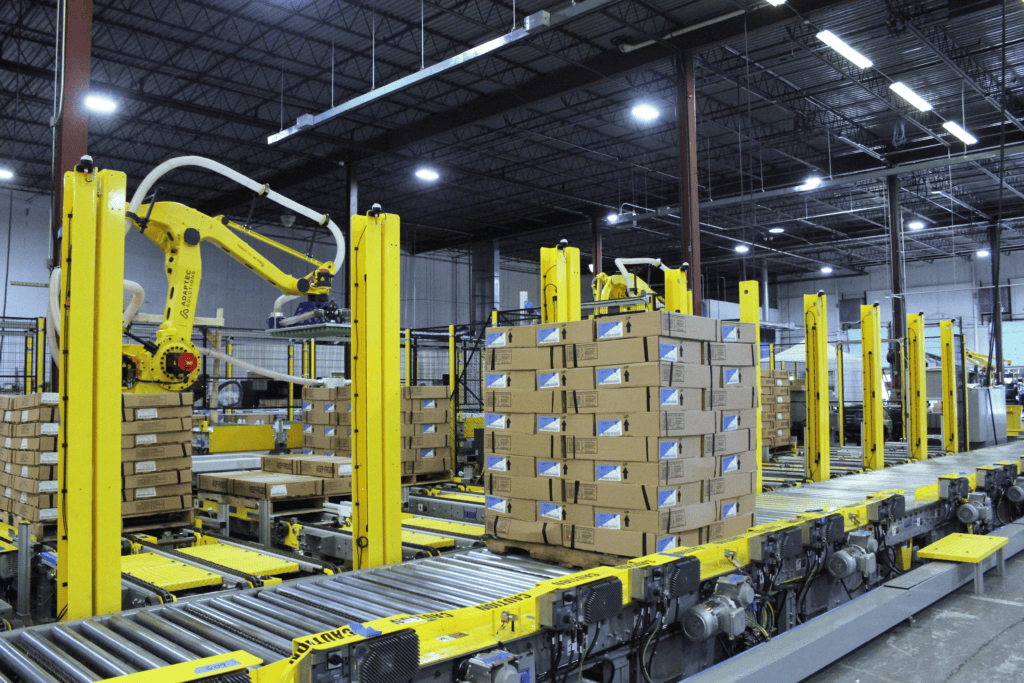
Pallet handling conveyors are designed to move pallets and other heavy-duty loads on belts, chains, skate wheels, or rollers. Pallet conveyors can be used to move large and heavy products with ease while maintaining safety. These systems are used to increase throughput for manufacturers and distributors utilizing large loads. Benefits include increased flexibility and safety with lowered cost of operations.
Main Usages
- Pallet Transfer Between Automated Processes
- Pallet Accumulation and Buffering
- Pallet Staging and Shipping Integration
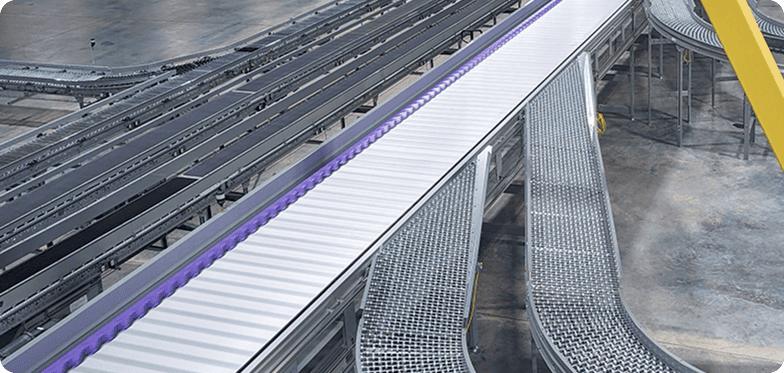
Sortation, merging and diverting conveyor systems are used to effectively sort products to other lines. Separating products from infeed conveyor lines to packing stations, palletizers, shipping lanes and other applications can be accomplished through these systems. Sortation conveyor systems utilize wheels, pushers or sliding shoes to achieve high throughput rates in a system.
We are able to create custom conveyor systems that sort and divert product based on shape, weight, line capacity and more. We can provide sortation solutions for all budget requirements through engineered design and integration of our conveyor partners: Hytrol, Dorner, Omni, Lewco.
Main Usages
- Order Fulfillment Routing
- Shipping Lane Distribution
- Product Classification and Sequencing
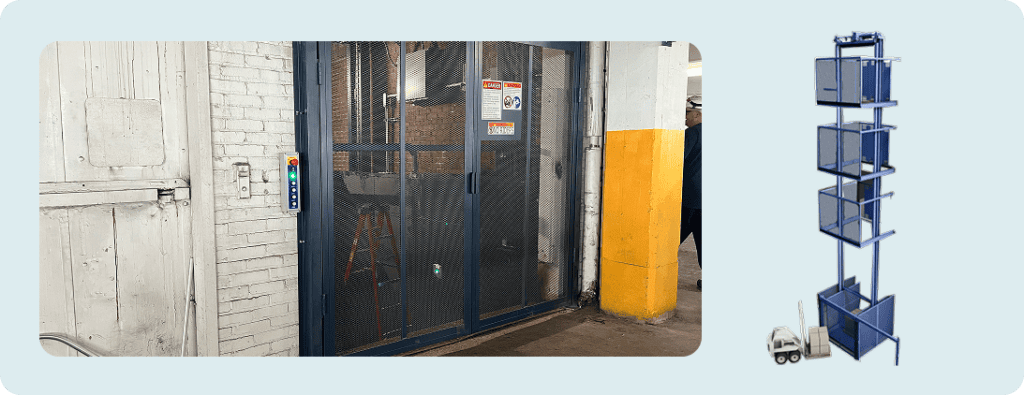
A Vertical Reciprocating Conveyor (VRC), also known as a material lift, is a type of material handling automation equipment that can move products between different levels in a vertical direction. VRCs provide a safe and efficient solution for transporting products to mezzanines, platforms, or between multiple floors in warehouses, distribution centers, manufacturing facilities, or other industrial settings.
Main Usages
- Multi-Level Material Transfer
- Work-In-Process (WIP) Flow
- Order Fulfillment and Storage Access
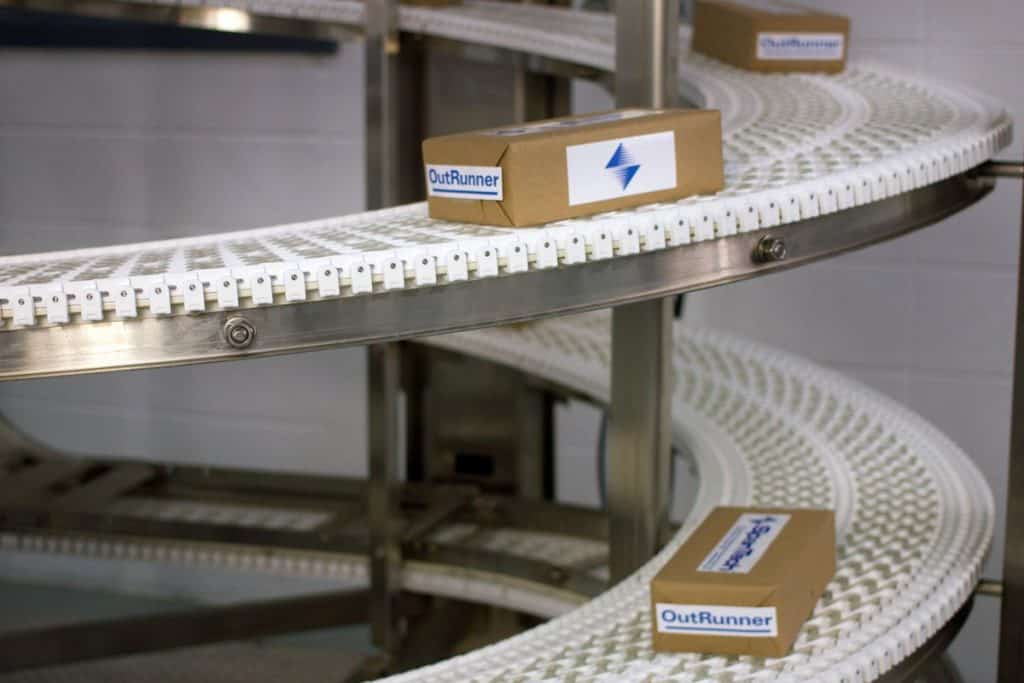
Spiral elevator conveyor and chutes are cost-effective solutions for changing elevations. Spirals take up a fraction of the floor space compared to other conveyor systems. For elevation change with a minimal footprint, spiral conveyors are an ideal, cost-effective solution.
Main Usages
- Elevating Products Between Levels
- Accumulation and Buffering
- Connecting Packaging and Distribution Systems
Integrated Components of a Conveyor System
Robotic Systems
Stretch Wrappers
Sortation Systems
Palletizers & Depalletizers
Warehouse Storage Systems
AMRs & AGVs
Why Choose Adaptec to Integrate your Conveyor System
Built Around Your Operation, Not Ours
We start with how your productuction moves, not a predefined solution. Every system is designed around your space, product mix, and flow so it works on your floor.
The Right Equipment, Not Just One Brand
We work across a network of proven conveyor technologies and partners to find what fits best. You get a system built for performance, not limited by a single product line.
Unmatched Skills of our Field Service Technicians
Our technicians understand the systems we install, so adjustments, expansions, and support happen quickly and accurately.
We partner with industry-leading conveyor brands to engineer your system.

Best-in-Class Service
Adaptec is built to keep you running. Our highly trained technicians maintain and optimize systems, helping prevent downtime and extend equipment life supporting your operation at every stage on its journey to greater efficiency.

Unmatched Technician Skill Sets

Spare Parts at Discounted Rates

24/7/365 Support
Explore Our Related Capabilities


Let’s Connect
Get in touch for an introductory call with our team.
Fill out the form or call (800) 724-5794